Cat Carrier Pet Blogger: Product Reviews
A review programme needs 8-14 serialised units per launch drawn from the bulk run, held to dimensional tolerance of 2 mm and weight tolerance of 4 percent against the published spec sheet, with a documentation pack — spec sheet, test report, material declaration — shipped in the same carton. Review units must be pulled from bulk, not built separately.
A blogger review is the only form of product coverage in which the reader can check the manufacturer's numbers, and that changes what has to be manufactured. The review unit cannot be a hand-built showpiece; it has to be a unit pulled from the same lot the customer will receive, carrying the same tolerances, the same trim and the same documentation. This page sets out how that is specified: sample-to-bulk conformance limits, the measurement protocol behind them, the documentation pack that supports a published claim, and the allocation maths for a multi-SKU review matrix. It also covers what happens after publication, because a review that finds a defect generates a revision loop with its own cost and timeline. Commercial terms follow the standard programme: MOQ 500 pieces per colourway, prototypes in 6-10 working days, bulk production 35-50 days after sample approval, final random inspection to AQL 2.5, T/T 30/70 and FOB Xiamen. The additions for a review programme are in traceability, documentation and dispatch timing, all of which are cheap to specify and expensive to improvise.
The difference between one dog carrier factory and another is rarely the stitch count - it is whether the cat carrier pattern survives a 1.5x static load without permanent set.
The Review Unit Conformance Problem: Sample-to-Bulk Drift
The central manufacturing risk in a review programme is drift between the unit that was reviewed and the units that ship. It arises whenever a review sample is built separately from bulk — on a different line, from different material, by a different operator — and it is the reason a published review can be simultaneously accurate and misleading.
Drift has three measurable sources. Material drift is the largest: a fabric from a second dye lot, a foam from a second pour, or a hardware batch from a second plating run each introduce a measurable difference in colour, compression set or finish. Process drift is second: a unit assembled by a senior operator at sampling speed is measurably different from the same unit assembled on a line at rate, particularly in seam alignment and in foam placement. Specification drift is third and the most damaging, where a change made after sampling — a cheaper zipper, a thinner foam — is never reflected in the published review.
| Source | Typical magnitude | Detectable by reviewer | Control | Cost of control (USD) |
|---|---|---|---|---|
| Dye lot change | Delta-E 1.5-4.0 | Yes, in side-by-side photos | Single lot release, Delta-E 1.0 | 0.05-0.20 per unit |
| Foam batch change | 3-8% compression set | Only by measurement | Density certificate per batch | 0.02-0.08 per unit |
| Hardware plating run | 15-40 gloss units | Yes, visually | Finish call on trim spec | 0.03-0.12 per unit |
| Operator skill variance | 2-5 mm seam alignment | Yes, in detail photos | Line-built pre-production sample | 25-50 per sample |
| Post-sampling substitution | Whole component | Yes | Change control, re-sample trigger | 80-260 per event |
The control is procedural rather than technical. A review unit is pulled from bulk production by the inspector during final random inspection, not built in advance; it is serialised and its serial number is recorded against the lot; and the bill of materials is frozen at sample approval, with any later substitution triggering a re-sample rather than a note in an email.
The second procedural control is a retained reference. Two units from every production lot are retained for 24 months, so that a conformance question raised months after publication can be answered against a physical unit from the same lot rather than from memory. Retention costs 24-60 USD per lot and settles disputes that would otherwise run for weeks.
Change control is the discipline that makes the rest work. Any change to material, component, process or sub-supplier after sample approval is logged, and the log entry states whether a re-sample is required. In practice about one change in three requires one, and catching those is what keeps a published review true.
Conformance is achieved by pulling review units from bulk at inspection and freezing the bill of materials, not by building nicer samples.
Dimensional and Weight Tolerances a Reviewer Will Measure
A blogger review is distinctive in that the reviewer measures. Tape measures, kitchen scales and calipers appear in the published piece, and any published number that does not match the delivered product becomes the headline of the review. The tolerances therefore have to be specified as tightly as the process allows, and the published figures have to be derived from measurement rather than from the drawing.
The working tolerances for a soft cat carrier are 2 mm on principal external dimensions, 3 mm on internal dimensions, 4% on unit weight, and 1.5 mm on strap and handle lengths. Internal dimensions matter more than external, because the internal figure is what determines whether an animal fits, and because internal dimensions drift more: a lining seam allowance of 3 mm or a foam thickness variance of 2 mm changes the usable interior by 6-10 mm.
Weight tolerance is the figure most often missed. A unit quoted at 1.25 kg and delivered at 1.42 kg is a 13.6% variance and reads as a specification error. Most of that variance comes from foam and from hardware, not from fabric, so weight control is a foam density and trim specification exercise.
| Measurement | Tolerance | Primary variance source | Secondary source | Control method |
|---|---|---|---|---|
| External length, width, height | Plus or minus 2 mm | Cutting accuracy | Seam allowance | Computerised cutting, 1 mm |
| Internal length, width, height | Plus or minus 3 mm | Lining seam allowance | Foam thickness | Seam gauge, foam certificate |
| Unit weight | Plus or minus 4% | Foam density | Hardware substitution | Weighed release, 5 per lot |
| Strap length | Plus or minus 1.5 mm | Webbing cutting | Heat-cut variance | Length jig |
| Ventilation open area | Plus or minus 2 percentage points | Mesh aperture | Panel tension | Aperture gauge per roll |
| Mesh aperture | Plus or minus 0.15 mm | Weave variance | Roll tension | Optical check per roll |
Published figures should come from a measured average of five units, rounded conservatively, with the tolerance stated. That is a different practice from publishing the drawing dimension, and it is the difference between a review that confirms the specification and one that contradicts it.
The interior floor dimension deserves its own note, because it is the number that determines fit and the one most often overstated in the market. A soft-sided carrier with a padded floor loses 8-20 mm of internal height to the pad under load, so the published internal height should be the loaded figure, measured with a 4 kg distributed load on the floor panel, rather than the unloaded one.
Publish measured averages from five units with a stated tolerance; a drawing dimension is not a specification a reviewer can verify.
Documentation Pack: Spec Sheets, Test Reports and Declarations
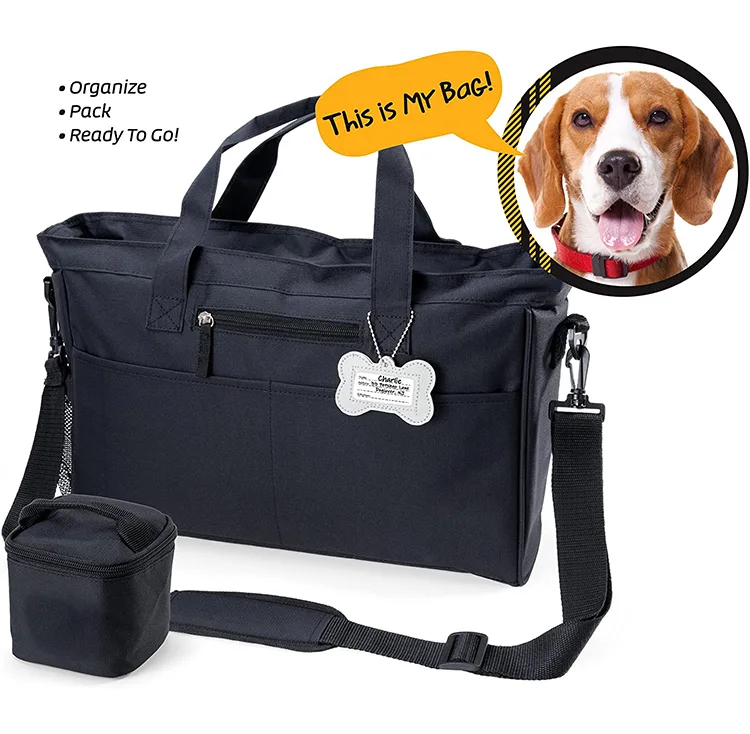
A review unit ships with paper as well as product. The documentation pack is what converts a reviewer's opinion into a verifiable claim, and its absence is the reason many otherwise competent reviews end with a hedge about unverified specifications.
The pack has four components. The specification sheet states dimensions, weight, materials by component, hardware specification and care instructions, with the tolerances from the previous section printed on it. The test report pack gives the actual measured results of the relevant tests, with the method, the sample count and the date. The material declaration covers restricted substances. The traceability card gives lot number, production date and serial number for the specific unit in the box.
Test reports are where manufacturers lose credibility most often, because a report that states a pass without a method or a sample size is not verifiable. A usable report states the method reference, the number of units tested, the conditioning, the measured values and the acceptance limit. A material declaration should reference recognised criteria rather than assert compliance, and textile declarations in this category are normally issued against OEKO-TEX criteria.
| Document | Contents | Pages | Production cost (USD) | Revision trigger |
|---|---|---|---|---|
| Specification sheet | Dimensions, weight, materials, tolerances | 1-2 | 0.04-0.12 | Any spec change |
| Test report pack | Method, sample count, measured values | 2-4 | 0.10-0.35 | Every 12 months or lot change |
| Material declaration | Restricted substance screening by component | 1-2 | 0.05-0.18 | Material or supplier change |
| Traceability card | Lot, date, serial, inspector ID | 1 | 0.02-0.06 | Every lot |
| Care and instruction leaflet | Cleaning, load limit, warranty | 2-4 | 0.08-0.30 | Regulatory or spec change |
Method references matter and they should be named. Textile and hardware test practice in this category follows published methods at ASTM International, and the quality system under which results are generated is certified to ISO 9001. A reviewer who wants to check a method can then do so, which is the whole point.
The traceability card is the smallest item in the pack and the most useful in a dispute. A unit with a lot number and a serial number can be traced back to its material lots, its line and its inspector within a day; a unit without one cannot be traced at all, and a quality question then becomes an argument about probabilities.
A review unit ships with five documents, and the test report is only useful if it names the method, the sample count and the measured values.
Colour and Finish Fidelity for Stills Photography
Stills photography in a review is unforgiving in a way video is not, because a still is examined rather than watched. The reviewer photographs the product on a surface, often beside a colour reference, often in daylight, and any deviation between the product and its online listing is visible in a single frame.
The controlling variables are the same three as in any colour-managed programme: dye lot, coating and substrate. What changes for a review is the tolerance and the number of reference points. Tolerance tightens to Delta-E 1.5 under D65 for the camera-facing panels and Delta-E 2.5 for interior and non-visible panels, and the number of reference points per production lot rises from three to eight.
Finish consistency is the second requirement and the one more often missed. A reviewer photographing two colourways side by side will see a gloss difference between two nominally identical finishes, because gloss varies with coating weight and cure. Specifying gloss as a range — 3-8 GU with all measured points within 4 GU of each other on a single unit — is what keeps a two-colour side-by-side from looking like two different products.
| Checkpoint | Illuminant | Tolerance | Points per lot | Action on fail |
|---|---|---|---|---|
| Camera-facing panel | D65 | Delta-E 1.5 | 8 | Hold lot, re-measure |
| Interior panel | D65 | Delta-E 2.5 | 4 | Note and release |
| Webbing and trim | D65 | Delta-E 2.0 | 4 | Hold trim lot |
| Gloss, exterior | 60 degrees | 3-8 GU, 4 GU spread | 6 | Hold lot |
| Panel-to-panel on one unit | D65 | Delta-E 1.0 | 5 units | Segregate units |
Packaging photography adds a fourth surface. A review almost always opens with the carton, and a carton printed from a different run, or a hang tag from a different print lot, will not match the product inside it. Packaging print should be released against the same tolerance as the product, at Delta-E 2.5, and cartons for review units should come from the main run rather than from a pre-production print.
The last fidelity item is creasing. A unit that ships folded arrives with fold lines that show in every photograph and that no amount of steaming fully removes. Review units should ship flat-packed in an over-box sized to the product's flat footprint, which adds 0.30-0.70 USD and removes the single most common complaint in review unboxings.
Fidelity for stills is a tighter tolerance and more measurement points, plus flat packing, because a photograph is examined rather than watched.
Multi-SKU Review Matrices and Sample Allocation
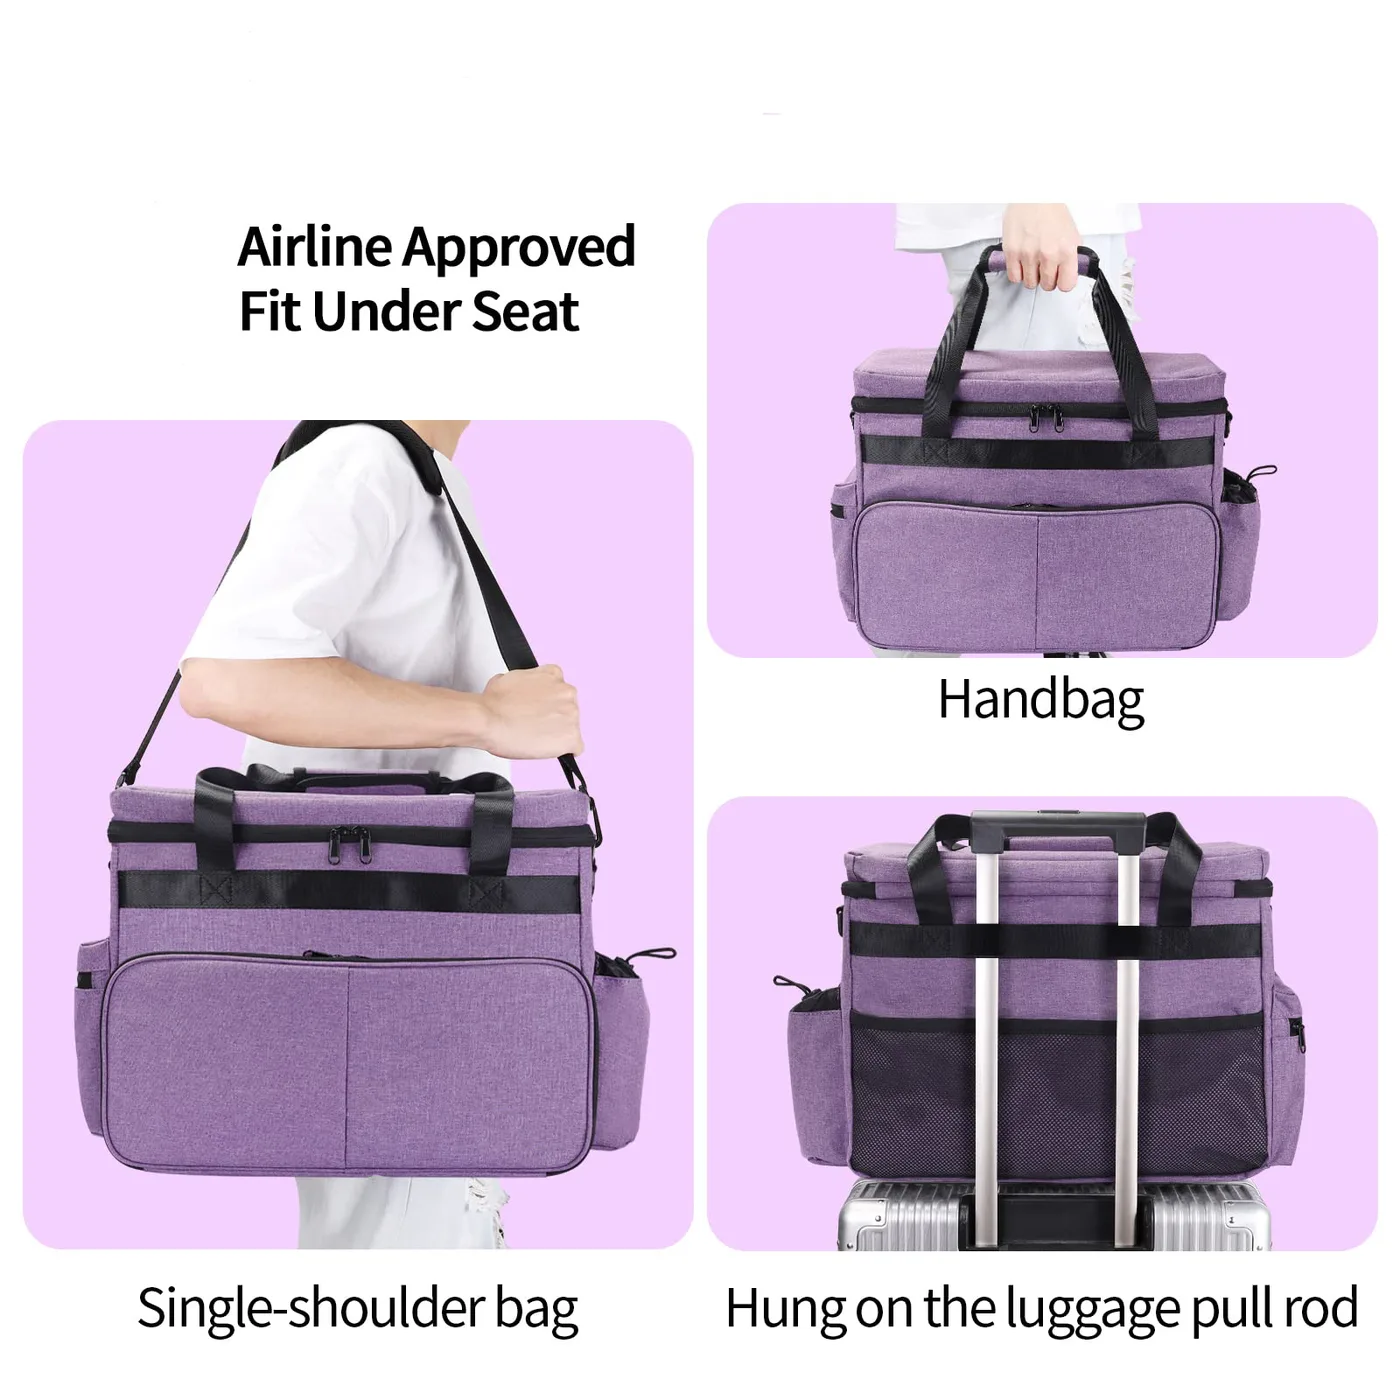
A blogger reviewing a range rather than a single unit needs a matrix, and the matrix has to be allocated before production rather than assembled afterwards. The allocation question is how many units of how many SKUs, and the answer is driven by what the review is intended to establish.
A single-product review needs 8-14 units: one primary review unit, two for photography variants, two for destructive or long-term testing, one retained reference, and 2-8 for a follow-up or a second reviewer. A range review across three sizes needs 4-6 per size, and a colourway review across four colours needs 3-4 per colourway, because colour is established by comparison and a single unit per colour cannot be compared against itself.
| Review type | SKUs covered | Units per SKU | Total units | Purpose split |
|---|---|---|---|---|
| Single product, single reviewer | 1 | 8 | 8 | 1 review, 2 photo, 2 test, 1 retain, 2 follow-up |
| Single product, two reviewers | 1 | 14 | 14 | 2 review, 4 photo, 3 test, 2 retain, 3 follow-up |
| Size range review | 3 | 5 | 15 | 1 review, 1 photo, 1 test, 1 retain, 1 follow-up |
| Colourway comparison | 4 | 3 | 12 | 1 review, 1 photo, 1 retain |
| Full launch, range and colour | 9 | 3 | 27 | 1 review, 1 photo, 1 retain |
Allocation interacts with MOQ in a way that surprises first-time programmes. A review matrix of 27 units drawn from a 1,500-unit order is 1.8% of the order and costs 400-700 USD at unit cost; the same matrix drawn as a separate pre-production run costs 45-120 USD per unit to build and cannot be sold. Drawing review units from bulk is both cheaper and more honest.
The retained reference units are the ones most often dropped from the allocation and should not be. Two units per lot held for 24 months, at 24-60 USD per lot, are what allow a conformance question raised eight months after publication to be answered with a measurement rather than an opinion.
Sequencing the dispatch is the last allocation decision. Staggering the matrix — review units first, photographic units two weeks later, follow-up units on request — keeps the reviewer's attention across a longer window and avoids all units arriving on one day and the review being written in a single session from a single unit.
Allocate the matrix in the purchase order, draw it from bulk, and never drop the retained references.
Sampling Rounds, Serialisation and Traceability
Sampling for a review programme runs three rounds with a specific output at each, and the third round is the one that differs from a standard programme: it produces the review units themselves rather than an approval sample.
Round one is the construction sample, 6-10 working days, evaluated for geometry and assembly. Round two is the colourway and trim sample, 6-10 working days, evaluated against the colour and finish criteria. Round three is the line-built pre-production sample, 6-10 working days, built on the production line from bulk materials — and from the same run, the review matrix units are pulled at final random inspection.
Serialisation is what makes the traceability work. Each review unit carries a serial label in a fixed location, normally the interior care label, encoding line, lot, date and unit sequence. The serial is recorded against the inspection record, so a question about one specific unit can be resolved against that unit's own inspection data.
| Stage | Duration | Units produced | Serialised | Held or dispatched |
|---|---|---|---|---|
| Round 1 construction sample | 6-10 working days | 1 | Yes | Held as reference |
| Round 2 colourway sample | 6-10 working days | 1 per colourway | Yes | Held as colour standard |
| Round 3 pre-production sample | 6-10 working days | 2-3 | Yes | 1 held, 1 dispatched for approval |
| Bulk production | 35-50 days | Full order | Lot level | Held pending inspection |
| Final random inspection, AQL 2.5 | 1-2 days | Sample per lot size | Recorded | Review units pulled here |
| Retained reference units | 24 months | 2 per lot | Yes | Held |
Inspection sample size follows the standard AQL 2.5 tables and is worth stating, because a reviewer who knows the sample size can judge the strength of a claim. At general inspection level II, a lot of 501-1,200 units takes a sample of 80 with 5 accepted defects; a lot of 1,201-3,200 takes 125 with 7; and a lot of 3,201-10,000 takes 200 with 10.
The sampling record is part of the documentation pack. A review unit that ships with its own inspection record — sample size, defects found, disposition — supports a stronger published claim than one that ships with a certificate alone.
Serialise at round one, pull review units at final inspection, and publish the AQL sample size alongside any quality claim.
Cost Model for a Review Sample Programme
A review programme adds cost in three places: the units themselves, the documentation, and the traceability overhead. None is large in absolute terms, and all three are cheaper specified up front than improvised later.
Units are the largest line. At a mid-specification unit cost of 14-20 USD, a 14-unit matrix costs 196-280 USD at unit cost, plus 60-140 USD of over-boxing and flat packing. A 27-unit range matrix costs 378-540 USD plus 110-190 USD packing. Against that, building the same units as separate pre-production samples costs 45-120 USD each, which is 630-3,240 USD for the same matrix.
Documentation is the second line and it is mostly fixed cost amortised over the run. A specification sheet is 120-320 USD to compose and 0.04-0.12 USD to print; a test report pack costs 180-600 USD in testing and 0.10-0.35 USD to reproduce; a material declaration is 90-260 USD per material set.
| Cost element | Fixed (USD) | Per unit (USD) | Total on 1,500 units (USD) | Notes |
|---|---|---|---|---|
| Matrix units at cost | 0 | 14-20 | 196-280 | Drawn from bulk |
| Flat pack and over-box, matrix only | 0 | 4-10 | 60-140 | Matrix units only |
| Serialisation labels | 40-90 | 0.02 | 70-120 | All units |
| Specification sheet | 120-320 | 0.04-0.12 | 180-500 | One-off composition |
| Test report pack | 180-600 | 0.10-0.35 | 330-1,125 | Annual refresh |
| Material declaration | 90-260 | 0.05-0.18 | 165-530 | Per material set |
| Retained reference units | 24-60 per lot | 0 | 48-120 | Two per lot, 24 months |
| Programme overhead total | 454-1,330 | 0.21-0.65 | 1,049-2,815 | Under 2 USD per unit |
The arithmetic to remember is that the whole programme adds 0.21-0.65 USD per unit across a 1,500-unit run, against a unit cost of 14-20 USD. That is 1.5-4.5% of unit cost for a materially stronger published claim, which makes a review programme one of the better-value additions available in this category.
Where it stops being cheap is when it is done late. Composing a specification sheet after production, or commissioning test reports after a review is published, costs 2-4 times the scheduled figure because the testing has to be expedited and the documentation has to be reconstructed from records rather than generated with the lot.
The programme adds under 2 USD per unit when scheduled, and three to four times that when assembled retrospectively.
Revision Loops After Publication: What Changes and What It Costs
A published review that finds a defect starts a revision loop, and the loop has a defined cost and timeline depending on which level of the product the finding sits at. Understanding the three levels is what makes the response fast rather than reactive.
Level one is a unit-level finding: one unit with a misaligned seam, a stiff zipper, a mark. It is resolved by inspection tightening and by replacing the unit, at 60-180 USD including freight, with no production change. Most review findings are at this level and most are handled in under a week.
Level two is a specification-level finding: the interior is 15 mm shorter than published, the pad compresses more than expected, the strap slips. It is resolved by a specification change and a re-sample, at 250-700 USD including a fresh sample round and updated documentation, on a 3-5 week path. It requires the published figures to be corrected, which is the part with reputational cost.
Level three is a component-level finding: a zipper that fails, a coating that abrades, a buckle that cracks. It is resolved by a component change, a re-sample, a re-test and possibly a field action on shipped units. Cost runs 900-4,500 USD depending on whether shipped stock is affected, and the timeline is 5-11 weeks.
| Level | Example finding | Response | Cost (USD) | Timeline | Production stop |
|---|---|---|---|---|---|
| 1 Unit | Misaligned seam on one unit | Inspection tightening, replacement | 60-180 | Under 1 week | No |
| 2 Specification | Interior 15 mm short of published | Spec change, re-sample, re-document | 250-700 | 3-5 weeks | No |
| 3 Component | Zipper fails at 800 cycles | Component change, re-test, possible field action | 900-4,500 | 5-11 weeks | Yes, 2-14 days |
| 3 plus field | Structural failure in use | Full recall and replacement run | 4,500-22,000 | 8-16 weeks | Yes |
The preventive measure is a pre-publication conformance check. Before a review unit leaves, it is measured against the published specification sheet and photographed under the release criteria, and any discrepancy is corrected in the documentation rather than in the product. That check costs 40-120 USD per launch and removes most level-two findings, which are the ones that cost credibility.
Response speed matters more than response cost. A manufacturer who acknowledges a finding with a measured response within 48 hours usually keeps the relationship and often gains a follow-up piece; one who argues about it for three weeks usually gets a second, less favourable mention.
Budget three response levels, and spend 40-120 USD on a pre-publication conformance check to avoid the middle one.
Freight and Timing for Review Unit Dispatch
Review units are dispatched on a schedule set by the reviewer, not by the production plan, and the dispatch decision is a choice between three modes with very different cost and certainty profiles.
Air express at 3-5 days and 12-22 USD per kg is the default for a matrix of 8-14 units. A 14-unit matrix at 1.2-1.6 kg packed, in four over-boxes, weighs 22-34 kg and costs 260-750 USD. That is 19-54 USD per unit, several times the unit cost, and it is correct whenever a publication date is fixed.
Air standard at 6-12 days and 7-14 USD per kg halves the cost and is correct when the review date is flexible by two weeks. Sea at 26-38 days and 0.75-2.40 USD per unit is only viable for review units when they travel with the main shipment, which means the review publishes after stock arrives — a perfectly workable plan for an evergreen review and a useless one for a launch review.
| Mode | Transit | Total cost (USD) | Per unit (USD) | Certainty | Use when |
|---|---|---|---|---|---|
| Air express | 3-5 days | 260-750 | 19-54 | High | Fixed publication date |
| Air standard | 6-12 days | 150-420 | 11-30 | Moderate | Two weeks of slack |
| Air consolidated | 8-15 days | 110-320 | 8-23 | Lower | Month of slack |
| Sea, with main shipment | 26-38 days | 18-42 | 1.30-3.00 | Moderate | Evergreen review, no date |
| Sea LCL, standalone | 28-38 days | 60-140 plus fees | 8-16 plus fees | Low | Almost never, minimum fees apply |
Customs documentation for review units is a frequent delay and it is avoidable. Review units have commercial value and are dutiable; shipping them marked as samples at zero value invites a hold. The correct treatment is a commercial invoice at the actual unit value with a clear description, which is what clears in 1-3 days rather than 1-3 weeks.
Timing the dispatch against the production calendar is the last piece. If review units are drawn at final inspection, they cannot leave before the bulk run completes, which on a 35-50 day run means the review publishes 40-60 days after sample approval. Where a review must publish earlier, the alternative is to dispatch round-three pre-production units by air and back-annotate the review with a note that units were pre-production — which is honest, and which most reviewers will state if asked.
Our production team schedules review matrices through the SGS-verified production base under ISO 9001 and BSCI coverage, with prototypes in 6-10 working days, bulk production 35-50 days after sample approval, final random inspection to AQL 2.5, T/T 30/70 and FOB Xiamen. Air express the matrix on a fixed date, invoice it at true value, and accept that a review drawn from bulk publishes 40-60 days after sample approval.
Production capability
- SGS-verified production space of 4,950 m², 149 machines, 7 assembly lines
- Pet carrier and pet bag output since 2014 from a 137-person team
- 200,000 units shipped monthly under BSCI and ISO 9001 systems
People Also Ask
Should review units be built separately or pulled from bulk?
Pulled from bulk at final random inspection. A separately built sample drifts on material, operator and specification, and costs 45-120 USD per unit against 14-20 USD drawn from the run.
What dimensional tolerance should a reviewable carrier hold?
2 mm on external dimensions, 3 mm on internal, 1.5 mm on strap lengths and 4% on weight. Internal figures drift most and should be measured under a 4 kg floor load.
What documents ship with a review unit?
A specification sheet with stated tolerances, a test report pack naming method and sample count, a material declaration, a traceability card with lot and serial, and a care leaflet.
How many units does a review matrix need?
8-14 for a single product, 4-6 per size for a size range, 3-4 per colourway for a colour comparison, and 3 per SKU for a full nine-SKU launch matrix.
What colour tolerance applies to review-facing production?
Delta-E 1.5 under D65 on camera-facing panels and Delta-E 2.5 on interiors, measured at eight points per lot rather than the usual three.
How is sample-to-bulk drift prevented?
By freezing the bill of materials at sample approval, logging every later change against a re-sample trigger, serialising units and retaining two references per lot for 24 months.
What does a review programme add to unit cost?
0.21-0.65 USD across a 1,500-unit run, or 1.5-4.5% of a 14-20 USD unit cost, covering serialisation, documentation, testing and retained references.
How should review units be declared to customs?
At true commercial value on a commercial invoice with a clear description. Zero-value sample declarations invite a hold and turn a 1-3 day clearance into 1-3 weeks.
Frequently Asked Questions
Why is material drift the largest source of sample-to-bulk difference?
A second dye lot shifts Delta-E by 1.5-4.0, a second foam pour shifts compression set by 3-8%, and a second plating run shifts gloss by 15-40 units. All three are visible in a side-by-side photograph.
Why do internal dimensions drift more than external ones?
Lining seam allowance and foam thickness both eat into the interior. A 3 mm seam allowance and a 2 mm foam variance together change usable internal space by 6-10 mm.
Why should published internal height be measured under load?
A padded floor loses 8-20 mm of internal height to pad compression under a 4 kg distributed load. Publishing the unloaded figure overstates the space an animal actually has.
What makes a test report verifiable by a reviewer?
A named method reference, the number of units tested, the conditioning, the measured values and the acceptance limit. A pass with no method or sample size cannot be checked.
How much does a retained reference programme cost?
24-60 USD per lot for two units held 24 months. It is what allows a conformance question raised eight months after publication to be answered with a measurement.
What is the AQL 2.5 sample size at common lot sizes?
At general inspection level II: 80 units sampled with 5 accepted for a 501-1,200 lot, 125 with 7 for 1,201-3,200, and 200 with 10 for 3,201-10,000.
Why should gloss be specified as a range rather than a maximum?
Two units at 4 GU and 9 GU both pass a maximum of 12 but look like different products side by side. Specifying a 4 GU spread within a single unit keeps a colourway comparison consistent.
Why do review units need flat packing?
Fold lines from a stuffed carton show in every photograph and steaming does not fully remove them. A flat-packed over-box adds 0.30-0.70 USD and removes the most common unboxing complaint.
How much of an order does a review matrix consume?
A 27-unit matrix from a 1,500-unit order is 1.8% of the run and costs 400-700 USD at unit cost, against 630-3,240 USD to build the same units separately.
What is a level-two revision finding?
A specification-level discrepancy such as an interior 15 mm shorter than published. It costs 250-700 USD, takes 3-5 weeks and requires the published figures to be corrected.
What is a level-three revision finding?
A component failure such as a zipper failing at 800 cycles. It costs 900-4,500 USD, takes 5-11 weeks, stops production for 2-14 days and may trigger a field action.
How much does a pre-publication conformance check cost?
40-120 USD per launch. It measures the unit against the published specification sheet before dispatch and removes most level-two findings, which are the ones that cost credibility.
Why is sea freight rarely used for review units?
At 26-38 days transit it only works when units travel with the main shipment, meaning the review publishes after stock lands. That suits an evergreen review and fails a launch review.
When should pre-production units be sent instead of bulk units?
When the review must publish before the 35-50 day bulk run completes. Send round-three units by air and state in the review that they were pre-production, which most reviewers will disclose if asked.
Talk to QUANZHOU JUNYUAN BAGS about a pet carrier program: MOQ 500 pieces per colourway, samples in 6-10 working days, bulk production in 35-50 days under AQL 2.5 inspection.
Get a free quote Request a sample