Pet Carrier Water Jug: Hydration
A 1.5-litre pet carrier water jug should use a documented food-contact PP or stainless reservoir, a 12-18 millimetre drinking outlet, and a valve that remains leak-free after 20,000 cycles. Specify 0.8-1.2 litres for cats and small dogs or 1.5-2.0 litres for medium dogs, then validate migration, flow, drop resistance, cleaning access and carrier attachment as one system.
A travel water jug is not simply a bottle placed beside a carrier. It is a fluid system exposed to vibration, temperature change, pressure variation and repeated contact with saliva. Product engineering therefore starts with the required drinking volume and journey profile, then moves through resin or steel selection, migration documentation, valve opening pressure, venting, mount stiffness and cleanability. A buyer should approve measurable targets: usable capacity within minus 3% to plus 5%, flow of 90-180 millilitres per minute, leakage below 1 gram after a four-hour vibration sequence, and no fracture after a 1.2-metre filled drop. The specification must also separate food-contact components from decorative housings so every wetted resin, seal, pigment and lubricant is traceable. Commercial planning remains straightforward: MOQ 500 pieces per colourway, samples in 6-10 working days, bulk production 35-50 days after approval, and final random inspection to AQL 2.5. T/T 30/70 and FOB Xiamen can be written into the purchase order. The following engineering framework lets brands compare jug concepts on water safety, carrier usability, test evidence and packed cube rather than on appearance alone.
Most buyers ask a pet bag supplier the same opening question: can the pet carrier accessory line be reordered in the original colour six months later? The answer depends on dye-lot control, not on goodwill.
Capacity and Hydration Duty Before Industrial Design
Capacity should be calculated from the trip, animal and refill opportunity before a shape is drawn. A compact carrier accessory can rarely hold an animal's entire daily demand without becoming unstable, so the practical design target is a travel reserve rather than a medical hydration promise. For cats and toy dogs, 0.8-1.2 litres normally balances duration and mass; for medium dogs, 1.5-2.0 litres is more useful. One litre of water adds one kilogram, which is significant on a soft carrier shoulder panel.
The stated volume, brimful volume and usable volume must be different fields in the tech pack. A nominal 1.5-litre body may have 1.62 litres at the brim but only 1.42 litres usable after headspace for shaking and thermal expansion. Accepting usable capacity at minus 3% to plus 5% prevents a narrow moulding tolerance from becoming a false claim. Graduations should be moulded or laser marked at 250-millilitre intervals and checked against a calibrated mass of water.
| Duty | Usable capacity | Filled mass | Outlet | Target flow | Mount load | Pack volume |
|---|---|---|---|---|---|---|
| Cat cabin trip | 0.75-0.90 L | 0.9-1.1 kg | 12 mm ball valve | 70-110 mL/min | 35 N | 1.5-2.0 L |
| Toy dog day trip | 0.90-1.20 L | 1.1-1.4 kg | 14 mm tray feed | 90-130 mL/min | 45 N | 1.8-2.6 L |
| Medium dog road trip | 1.50-2.00 L | 1.8-2.3 kg | 16-18 mm spout | 120-180 mL/min | 70 N | 2.8-4.2 L |
| Crate-mounted reserve | 2.00-3.00 L | 2.3-3.4 kg | 18 mm gravity valve | 140-220 mL/min | 90 N | 4.0-5.8 L |
Mount load is more informative than empty product weight. A filled jug can produce two to three times its static load when a vehicle hits a bump, so a 1.5-kilogram assembly should be designed around at least 45 newtons at the bracket and 90 newtons as a short proof load. That figure belongs on the carrier-side specification as well as on the jug drawing.
Shape follows this duty calculation. A broad 72-88 millimetre body is easier to clean and less likely to tip, while a narrow 55-65 millimetre bottle fits pockets but needs internal ribs to control panel collapse. The buyer should approve a capacity-and-load sheet before approving colour or graphics. A carrier water jug is correctly sized when usable volume, filled mass and dynamic mount load are specified together.
Food-Contact Material Stack and Migration Control
Every component touched by water belongs in the food-contact bill of materials: reservoir, cap, spout, ball, spring, gasket, vent membrane, adhesive and any process lubricant. A common construction uses injection- or blow-moulded polypropylene for the body, a 304 stainless spring, a platinum-cured silicone gasket and a PP cap. A premium version uses a 304 or 316 stainless reservoir with a moulded PP drinking head. Mixing undocumented colour masterbatch into an otherwise compliant resin invalidates the material package.
Polypropylene is appropriate because it has low density, useful hinge fatigue and good resistance to normal cleaning chemistry. A body wall of 1.4-2.2 millimetres with ribs at 18-30 millimetre pitch limits oil-canning without excessive resin. Tritan-type copolyester gives clarity but requires a separate declaration for the exact grade. Silicone seals should be specified by cure system, hardness of Shore A 45-60, post-cure condition and colour formulation rather than merely described as food grade.
Migration verification should reproduce intended use. For ambient water, the laboratory plan records contact time, temperature, surface-area-to-volume ratio and repeated-use cycles. Overall and specific migration limits are market-dependent, so the purchase specification should name the destination rule and test simulant rather than copy a generic pass statement. A declaration from the resin supplier, formulation disclosure for pigments and a test report on the finished wetted assembly form a defensible file.
Restricted-substance review remains separate from migration. The European chemicals framework maintained by ECHA informs substance screening, while California exposure assessment can be checked against the lists maintained by OEHHA. Neither homepage replaces product-specific legal review, but both are authoritative starting points for the compliance matrix.
Incoming controls prevent substitutions after approval. Resin lot number, melt-flow range, seal hardness and steel grade should be recorded per batch. Our production team retains the approved golden sample and weighs each moulded body to catch wall thinning. Food-contact compliance belongs to the exact wetted assembly and intended contact condition, not to a vague material name on a quotation.
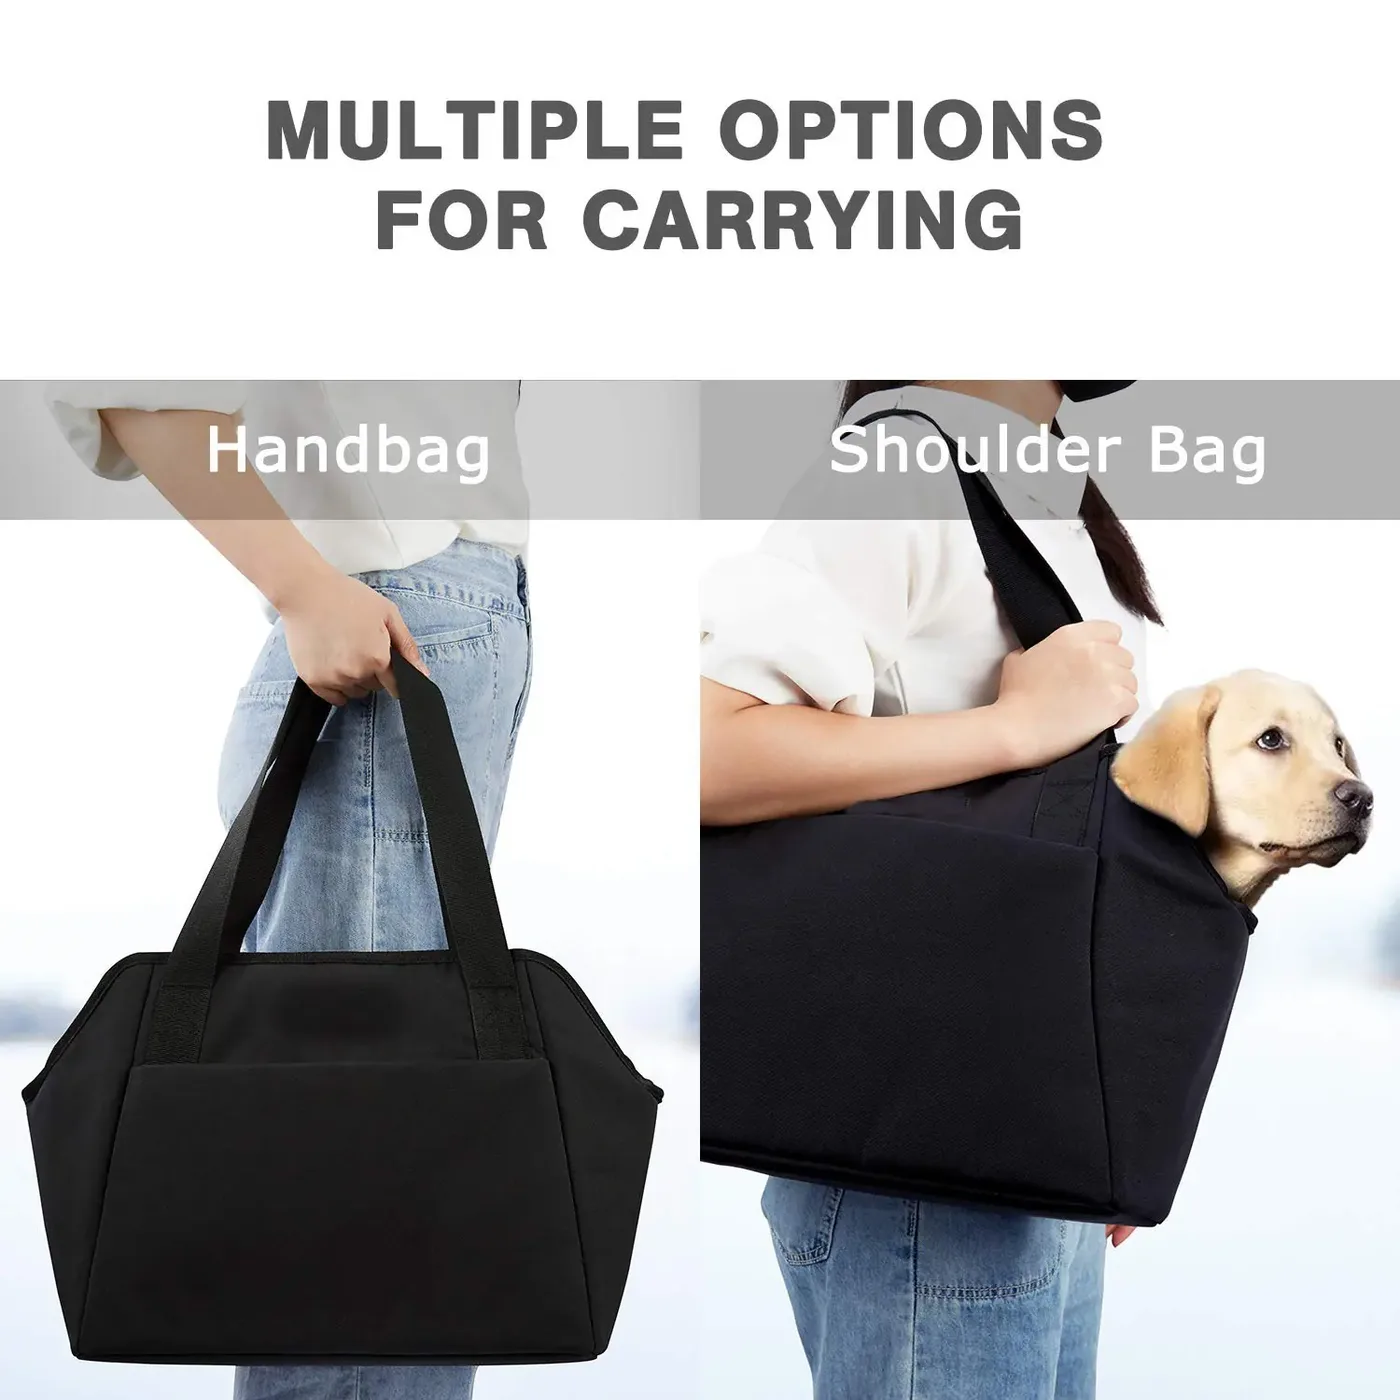
Valve, Vent and Flow Engineering Without Drips
A travel jug must admit air as water leaves; otherwise flow slows, stops or arrives in pulses. The valve and vent therefore work as a pair. A ball outlet may use gravity and tongue contact, while a tray-fed spout opens through a button or tilt action. For most carrier use, 90-180 millilitres per minute is fast enough for drinking but slow enough to avoid splashing in a moving vehicle.
Opening force is a pet-interface dimension. A ball valve for a cat or toy dog should begin movement at 0.8-1.5 newtons and deliver full flow by 2.0 newtons. A larger dog can operate 1.5-2.8 newtons. Too little preload creates transport drips; too much turns hydration into work. Spring wire diameter, ball diameter, seat angle and silicone lip compression must be controlled on the component drawing because each shifts opening force.
Vent choice affects both hygiene and leakage. A simple pinhole of 0.5-0.9 millimetres flows well but can wet the cap during inversion. A hydrophobic membrane passes air while resisting water, yet it can clog with mineral residue and needs a protected seat. A one-way silicone duckbill is washable and economical, provided its slit opening and wall thickness are gauged. The vent should be replaceable or accessible without a sharp tool.
Leak tests need several orientations. A filled jug is held upright, on each side and inverted for 60 minutes, then vibrated for four hours at the packed configuration. Acceptance can be set below 1 gram of mass loss, with no free droplet on tissue at the outlet. A thermal sequence from 5 to 45 degrees Celsius reveals pressure-driven leakage that a room-temperature test misses. Valve endurance then runs 20,000 operating cycles, followed by the same leakage and flow measurements.
Seat finish matters more than nominal valve material. A mould parting line crossing the seal can create a channel only 0.03 millimetres deep and still leak. The tool should put the gate and parting line away from the sealing land, and cavity inspection should include magnification. A no-drip claim is credible only when opening force, flow, inversion loss, vibration loss and post-cycle performance are all measured.
Housing Ribs, Drop Strength and Carrier Attachment
The reservoir wall must resist three different loads: internal pressure from temperature change, impact from a filled drop and local compression from a bracket. A thin smooth bottle that looks rigid when empty can crease permanently when a clamp is tightened. Circumferential ribs 1.0-1.8 millimetres high at 18-30 millimetre spacing raise panel stiffness without increasing the entire wall, while vertical ribs control buckling near the mount.
Rib location should follow stress rather than styling. Keep a smooth label zone where graphics are applied, but place two reinforced bands under the upper and lower bracket contacts. Around a threaded neck, use a shoulder radius of 3-6 millimetres and radial gussets that fade gradually into the body. An abrupt thick-to-thin transition creates sink on the outside and residual stress on the inside.
Drop qualification uses the filled product because water inertia drives the failure. A practical sequence is one drop each on base, side and cap from 1.2 metres onto a rigid surface at 23 degrees, followed by a cold-conditioned sequence at 5 degrees. Acceptance is no fracture, no cap release and leakage below 1 gram over the next hour. The test should be repeated on the lowest resin weight allowed by tolerance, not only on a heavy pilot sample.
Attachment can be by pocket, strap cradle, wire clip or bolted crate bracket. A pocket spreads load but may trap moisture; a strap is adaptable but can swing; a rigid bracket controls motion but concentrates force. For a 1.5-litre jug, specify a 45-newton working load, a 90-newton proof load for ten seconds and less than 8 millimetres of displacement at the outlet. Carrier fabric attachments need reinforcement patches extending 25-40 millimetres beyond the mount.
A tether is not a substitute for a bracket, but it is useful secondary retention. A 15-20 millimetre webbing loop rated above 250 newtons prevents a detached jug becoming a projectile. Our production team checks bracket fit with the actual carrier panel, not a flat coupon. The filled drop and dynamic mount proof are the governing structural tests; empty-bottle inspection cannot predict travel performance.
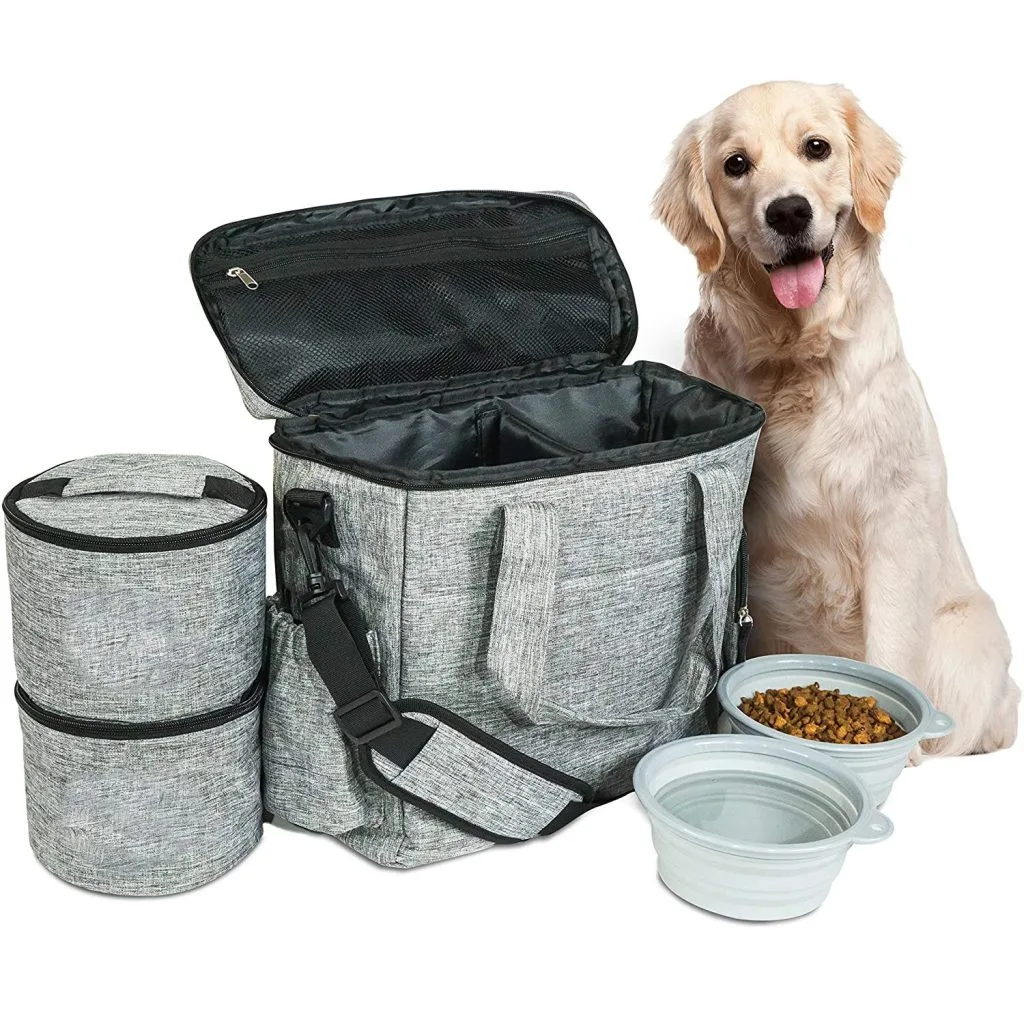
Cleaning Access, Biofilm Risk and Replaceable Seals
Cleanability is a geometric property. A reservoir that cannot accept a 35-45 millimetre cleaning brush, a cap with blind pockets, or a valve that requires pliers to dismantle will accumulate residue regardless of the resin declaration. The main opening should be at least 42 millimetres for compact models and 55 millimetres for larger ones, with internal corner radii above 4 millimetres and no enclosed channel narrower than the supplied brush.
The wetted path should separate into no more than five user-service parts: reservoir, cap, valve body, seal and ball or tray. More pieces increase loss and incorrect reassembly; fewer pieces often conceal a cavity. Alignment marks and asymmetric features can prevent a silicone valve from being installed backwards. A spare seal packed in a labelled paper envelope costs little and extends the service life of the jug.
Surface condition is as important as access. A moulded PP interior should avoid heavy texture below the water line, and a stainless interior should have a smooth, cleanable finish with weld tint removed. Scratches and undercuts hold organic residue. Dishwasher claims must name rack position, detergent and cycle temperature; otherwise the safer instruction is hand washing below the validated temperature.
A cleaning validation can use a visible soil containing protein and colour, a prescribed wash, and inspection under white and ultraviolet light. The engineering goal is no visible residue in the valve seat, vent recess or thread root after five soil-and-wash cycles. A dimensional check follows 25 and 100 cleaning cycles because cap ovality or seal compression can create leakage even when the product still looks intact.
Drying is the overlooked half of cleaning. Components should stand open without trapping a sealed water pocket, and the cap should include a draining orientation. Avoid absorbent foam inside the wetted assembly. Instructions should tell users to empty after travel, disassemble, wash and air dry completely. A wide opening and tool-free five-part water path prevent contamination more reliably than an antimicrobial marketing claim.
Temperature, Pressure and Transport Environment
A closed jug experiences pressure changes even when it is not used. Water and trapped air expand in a warm vehicle, cabin pressure changes during flight, and a cold reservoir makes seals less flexible. The design should not promise suitability for a transport mode until it has been tested through the relevant pressure and temperature envelope with the intended fill level.
Headspace provides the first control. Filling to 90-94% of brimful volume leaves enough air space for thermal expansion and movement. The moulded maximum-fill line should be visible from the filling position and remain legible after abrasion. A pressure-relief feature may be needed on a large rigid reservoir, but it must open above normal transport pressure and below body damage pressure without creating a routine drip path.
A useful thermal protocol holds filled samples at 5 degrees Celsius for four hours, 23 degrees for two hours and 45 degrees for four hours, then repeats the sequence three times. The assembly is weighed before and after each stage, the cap torque is recorded, and the body is checked for permanent panel distortion. Silicone seals at Shore A 45-60 normally maintain compliance over this range when compression is correctly set.
Pressure testing can be conducted with controlled air above water so leaks are visible. A proof pressure of 20-35 kilopascals for ten minutes is appropriate for a non-carbonated travel jug design target, followed by a leak check at normal pressure. This is not a universal regulatory figure; it is a buyer-defined performance level that should be adjusted to the intended route and validated by the responsible laboratory.
Hot liquids should be excluded unless the complete assembly is designed and labelled for them. Elevated liquid temperature changes migration, softens thermoplastics and creates a scald hazard at the drinking head. A normal pet hydration jug should state ambient or cool water only. Designing around 90-94% fill, 5-45 degree conditioning and a defined proof pressure controls the transport leaks that room-temperature inspection misses.
Carton Cube, Nesting and Retail Presentation
A rigid reservoir ships mostly air unless the jug is designed to nest or the body and head are packed separately. Packaging therefore starts during industrial design rather than after tooling. A tapered body with 1.0-2.5 degrees of draft can nest 35-55% of its height, while a straight cylinder cannot. Detaching the drinking head may reduce cube further, but it adds an assembly step and a risk of the customer fitting the seal incorrectly.
For a 1.2-litre jug, a non-nested retail box may occupy 3.0-4.0 litres. Controlled nesting can reduce shipping cube to 1.8-2.5 litres per unit in a master carton, saving 25-45%. Contact points need removable tissue or a thin recyclable sleeve so moulded surfaces do not scuff. A positive stop prevents one body wedging into the next under carton compression.
Master cartons should be designed against filled volume and actual pallet pattern, not a nominal unit dimension. Common targets are 12-24 units, gross mass below 15 kilograms for manual handling, and unused void below 10%. Divider count, cap orientation and accessory envelope location should be fixed on the packing instruction. A loose steel bracket can scratch every body in a carton during vibration.
Retail presentation has to show cleaning and assembly without enlarging the pack. A line drawing on the carton can explain the valve, maximum fill and disassembly sequence; a QR code may supplement but should not replace required instructions. Material identification and lot traceability should remain visible after the outer carton is discarded.
Pack verification combines compression, vibration and a drop in distribution configuration. The jug is then checked for cosmetic scuffing, thread damage, missing parts and leakage after reassembly. ASTM maintains a broad catalogue of packaging and material test methods at ASTM International; the exact method and severity should be named in the buyer's protocol. A nestable body and locked accessory location can remove 25-45% of shipping cube without changing usable water capacity.
Sampling, Quality Gates and Purchase Specification
The development path should answer one technical question at each gate. A concept sample confirms volume, pet access and carrier position. An engineering sample confirms tool geometry, valve opening force and cleaning. A pre-production sample uses nominated production materials and packaging. Approval of a hand-built model should never be treated as approval of moulded performance because gate position, shrinkage and seal finish appear only in production tooling.
The control plan needs variable data, not only pass or fail. Record body mass, wall thickness at six locations, neck ovality, cap application torque, valve opening force, flow, four-orientation leakage and bracket displacement. Plotting these readings by cavity identifies a drifting tool before leakage becomes an AQL defect. Cavities should be marked discreetly on the part for traceability.
Food-contact documents are reviewed before material release. The exact resin grade, colour masterbatch, silicone formulation, stainless grade and any lubricant must match the approved bill. Quality management can be organized under the process principles described by ISO 9001, while actual product acceptance remains defined by the purchase specification and laboratory reports.
Final random inspection to AQL 2.5 covers appearance, assembly, dimensions, marking and functional tests chosen for the lot. Critical leakage or sharp-edge failures should be treated separately with a tighter acceptance rule agreed before production. Retain samples from the first, middle and final shift, and retain one sealed material-document set for reorders.
Commercial fields belong beside the engineering fields: MOQ 500 pieces per colourway, samples in 6-10 working days, bulk production 35-50 days after signed approval, T/T 30/70 and FOB Xiamen. The SGS-verified production base supports documented lot control, while our production team coordinates carrier-side fit checks and shipment records. Each shipment file should also include the approved packing diagram, signed inspection summary, current compliance declarations and a clear reconciliation between ordered colours, mould cavities, carton marks and retained samples. A purchase specification is complete only when capacity, wetted BOM, flow, leakage, cleaning, mount load, packing and inspection evidence are all tied to revision-controlled drawings.
Order and quality terms
- MOQ 500 pieces per colourway; samples in 6-10 working days
- Bulk production 35-50 days after approval; AQL 2.5 inspection standard
- T/T 30/70 terms, FOB Xiamen, full document set per shipment
People Also Ask
What size water jug works with a pet carrier?
Use 0.8-1.2 litres for cats and toy dogs or 1.5-2.0 litres for medium dogs. Confirm the filled mass and carrier mount load before selecting capacity.
How fast should a pet water jug dispense?
A practical target is 90-180 millilitres per minute. Small-animal ball valves can start opening at 0.8-1.5 N, while larger outlets may use 1.5-2.8 N.
Which materials are suitable for the wetted parts?
Documented food-contact PP, 304 or 316 stainless steel, and platinum-cured silicone are common choices. The exact grade, pigment, lubricant and intended contact condition must be declared.
How is a travel jug checked for leaks?
Weigh it before and after upright, side and inverted holds, then run four hours of packed vibration. A useful buyer target is less than 1 gram lost with no free droplet.
Can a pet water jug carry hot water?
Not unless the complete assembly is specifically designed, migration-tested and labelled for hot liquids. Standard travel jugs should be limited to ambient or cool water.
How much carton space can nesting save?
A tapered body nesting 35-55% of its height can reduce master-carton cube by about 25-45%, provided positive stops and scuff protection are built into the pack.
Frequently Asked Questions
Why must usable capacity differ from brimful capacity?
Headspace is needed for shaking and thermal expansion. A 1.5-litre nominal body may provide about 1.42 litres usable while holding 1.62 litres at the brim.
What wall thickness works for a PP reservoir?
A 1.4-2.2 mm wall with ribs 1.0-1.8 mm high at 18-30 mm pitch is a useful starting specification, refined by tool flow and filled-drop testing.
Why does a jug need an air vent?
Air must replace dispensed water. Without a controlled vent, the flow slows, stops or pulses; an oversized vent can instead create an inversion leak.
What is the purpose of valve cycle testing?
It reveals spring relaxation, ball-seat wear and silicone compression set. Repeating flow and leakage tests after 20,000 cycles verifies that performance survives use.
How strong should the carrier bracket be?
For a 1.5-litre assembly, a 45 N working load and 90 N ten-second proof load are practical targets, with outlet displacement held below 8 mm.
Why test a jug while it is filled?
Water inertia drives impact and bracket loads. An empty bottle can survive a 1.2 m drop while the same body cracks or releases its cap when full.
How wide should the cleaning opening be?
At least 42 mm for compact models and about 55 mm for larger reservoirs, with internal radii above 4 mm and access for a 35-45 mm brush.
Are antimicrobial additives a substitute for cleaning?
No. Wide access, disassembly, washing and complete air drying control residue more reliably. Any antimicrobial claim also needs separate substantiation.
Why specify a maximum-fill line?
Filling to 90-94% of brimful volume leaves expansion headspace and reduces pressure-driven leakage during warm transport.
What causes leakage at an apparently good valve?
A mould parting line or gate mark crossing the sealing land can make a microscopic channel. Tool layout and magnified cavity inspection control that defect.
Should the jug head be packed assembled?
Assembly reduces user error but increases cube. Separate packing is acceptable when keyed geometry, clear instructions and a protected seal make incorrect fitting unlikely.
Which production records should be retained?
Keep resin and seal lots, cavity data, dimensional readings, opening force, flow, leak results, packing checks and first-middle-last shift samples.
Talk to QUANZHOU JUNYUAN BAGS about a pet carrier program: MOQ 500 pieces per colourway, samples in 6-10 working days, bulk production in 35-50 days under AQL 2.5 inspection.
Get a free quote Request a sample